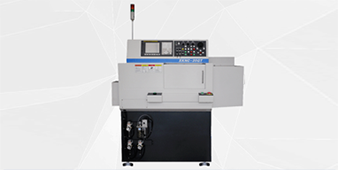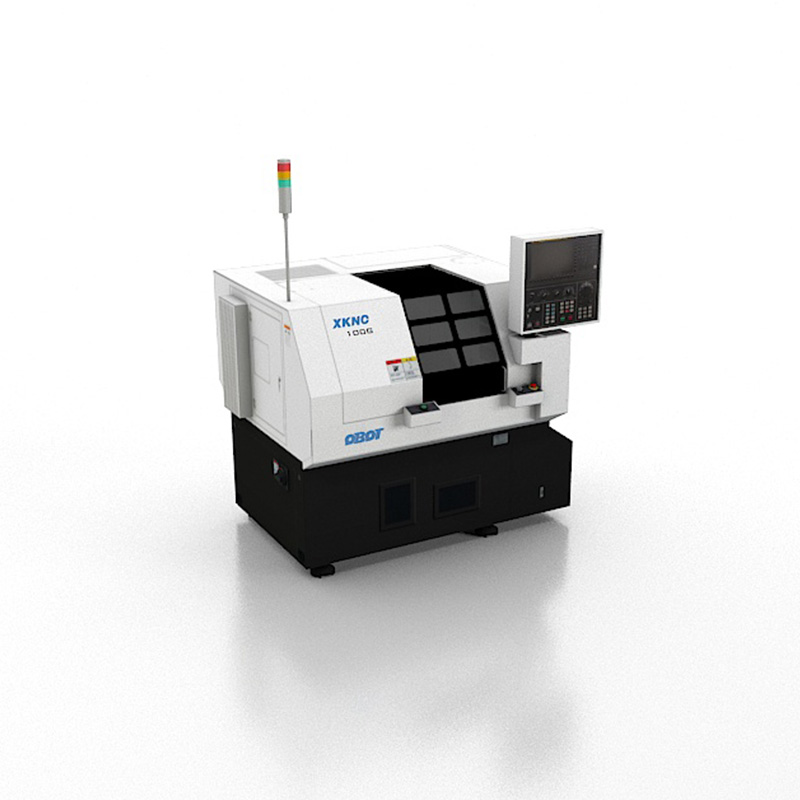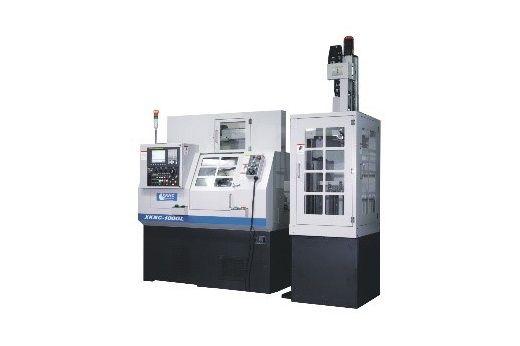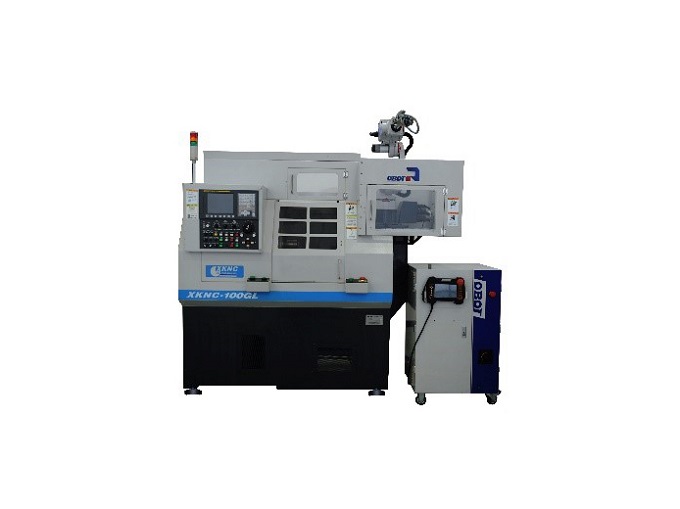
XKNC-100G series
The Z-axis of this machine adopts double-mount sliding guide rails, and is equipped with a variety of options such as spindle-enhanced spring chucks and chucks. On the basis of high precision, it can truly meet the needs of automated processing with a large processing range and high rigidity. Claim. Optional power tool and Cs contour control processing function. Abundant flexible machining combinations make it possible to "compound machining = one clamping" on a gang tool lathe.
1.guide

1. Extend the scraping technology and super-fine grinding process of the Japanese village of Bukchon for centuries, and configure the automatic lubrication system to ensure long-term high precision and high stability of the machine.
2. Using the dovetail rail structure, HT300 material, its high strength, good wear resistance, excellent overall design, excellent shock absorption effect, to ensure that the machine tool has higher rigidity in the case of high precision machining.

1. The Z-axis adopts the double-mount type sliding guide rail, which truly meets the automatic processing with high rigidity and large processing range.
2. The hard rail structure, the contact surface is subjected to scraping treatment, the more the average number of scraping points per square inch is 12-14 points, the rigidity is naturally improved.
2.Bed structure

1. The bed is a rigid structure with a rigid structure. The main shaft and the Z-axis are located in the middle of the bed, which effectively reduces the influence of the thermal clamping position on the position accuracy.
2. HT300 material, its high strength, good wear resistance, excellent overall design, excellent shock absorption effect.
3.High-precision spindle

1. Shaft core: It uses unique spindle material, after multiple heat treatment and fine processing, with stronger impact resistance and wear resistance. .
2. Bearing: the use of imported brand high-precision ball bearings, using P4 level, lifetime maintenance-free.
3. Waterproof: use imported advanced waterproof ring.

1. Optional built-in electric spindle, Ф30 specification spindle speed 8000rpm, Ф42 specification spindle speed 6000rpm, using oil heat exchanger cooling to ensure high speed and high precision of the spindle, greatly improving production efficiency.
2. The diameter of the through hole of the main shaft is D38mm and the maximum speed is 4500rpm. The diameter of the through hole of the main shaft is D25mm and the maximum speed is 6000rpm.
4.operating system
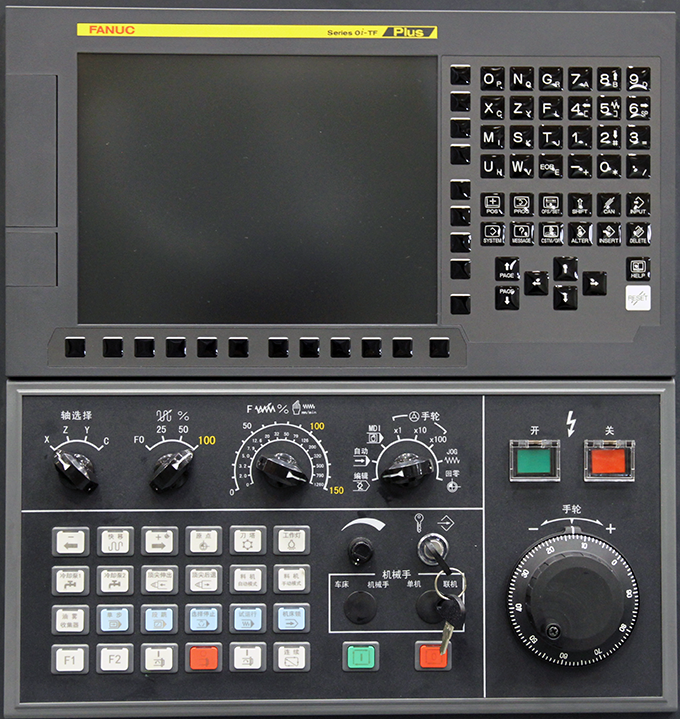
FANUC operating system
1. High speed and high precision rigid tapping.
2. Composite machining cycle that simplifies lathe programming.
3. Cylindrical interpolation function, which can be programmed according to the developed view of the cylindrical surface.
4. Direct size programming simplifies the programming of part program.
5. Memory pitch error compensation can compensate the error in mechanical system such as screw pitch error. The compensation data is stored in the memory of CNC in the form of parameters.
6. The CNC has built-in PMC programming function to control the machine and external equipment.
7. Random memory module, which can directly change the PMC program and macro executor program on the CNC.
5.Reasonable gang tool structure

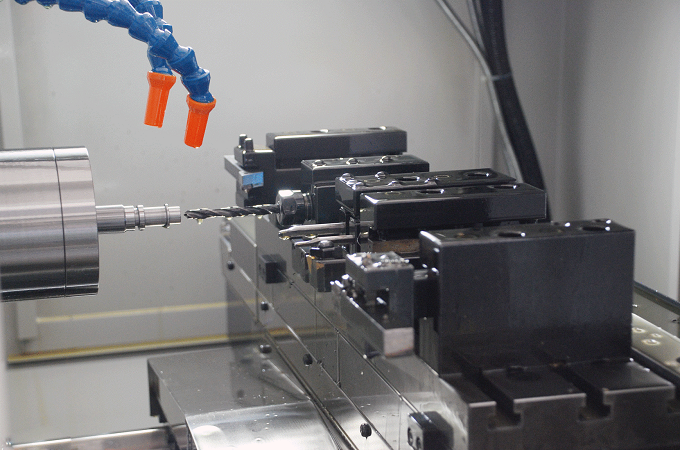
The machine is equipped with the proper mutation structure and sufficient tool installation space The precise machining tools for drilling, thread tapping, internal boring, turning Radial drilling threading and cutting can be installed in the tool post.
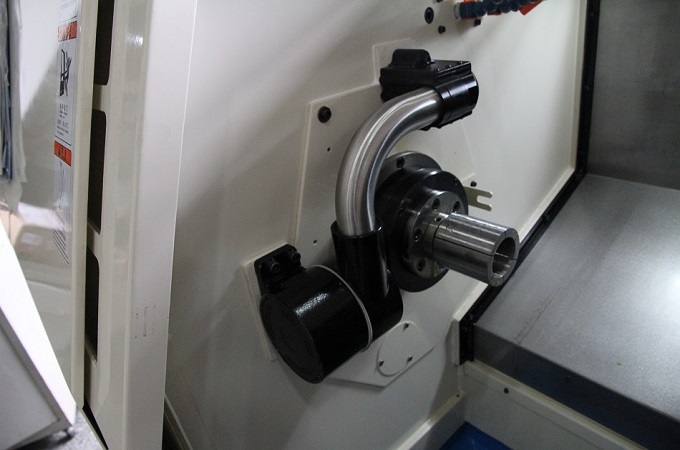
6.A variety of automatic clamp opening and closing and clamping device options
Hydraulic rotary cylinder:
1. The process is stable and easy to absorb shock and vibration.
2, the clamping force is large, easy to achieve stepless speed regulation, the speed range is large.
3. The imported hydraulic station has reliable pressure retention, high efficiency and simple structure.

Hydraulic rotary cylinder

Hydraulic station
Pneumatic rotary cylinder:
1. Simple operation, easy and automatic.
2. Fast response and improve production efficiency.
3, optional chuck clamping method, accurate clamping, large clamping range.

Pneumatic rotary cylinder
7.High-pressure internal cooling device

It can effectively cool lubrication and improve efficiency to ensure product quality.
8.Oil mist collection device

Reduce pollution and improve the working environment.
9.Chip conveyor

The iron scraps produced by the parts are automatically discharged out of the machine and are suitable for automatic machining and large chips.
10.Tool setter

Accurate measurement and easy operation. The contact type CNC lathe blade sensor can detect the precise position, wear and tear of the turning blade, and automatically correct the wear amount.
11.CS axis contour control

It can realize related functions such as surface, indexing and compound processing.
12.automation


Servo robotic hand-feeding device/robot automatic loading and unloading device
13.Parts transfer device + feeder interface

After the parts are processed, the machine door can be opened directly without passing through the machine door, and then directly to the machine outside receiving box through the parts conveying device, which improves the efficiency.
14.Clamping detection device

High-precision sensor detection is sensitive, ensuring good clamping and improving production quality.
15.Cutting oil device

It is used to store the coolant and is equipped with a cooling pump to achieve circulation of the coolant circuit.
16.Automatic feeder

Reduce downtime and greatly increase production efficiency, but require higher bar stock.
(1)机械本体标准规格MACHINE SPECIFICATIONS | ||||
项目Item | 100G(Φ38) | 100G(Φ25) | 100GS(Φ25) | |
加工能力 Capacity | 床身上最大回转直径Swing over bed | Φ320mm | ||
刀座底板上回转直径 Swing over cross slide | Φ160mm | |||
最大加工直径Max. machining diameter | Φ150mm | Φ125mm | Φ100mm | |
最大加工长度Max. machining length | 100mm | |||
主轴 Spindle | 主轴速度Spindle speed | Max.4500r/min | Max.6000r/min | Max.6000r/min |
主轴通孔直径Through hole diameter | Φ38mm | Φ25mm | Φ25mm | |
回转速度变换Number of speed ranges | 无级(S指令)Step-less | |||
副主轴轴速度Sub spindle speed | - | - | Max.6000r/min | |
副主轴通孔直径 Sub spindle Through hole diameter | - | - | Φ20mm | |
副主轴速度变换 Number of Sub spindle speed ranges | - | - | 无级(S指令)Step-less | |
主轴中心高 Height from floor to spindle center | 1070mm | |||
刀塔 Turret | 8工位(槽刀盘) 8positions(Grooving tool disc) | - | - | 16mm×16mm |
轴向刀座Axis tool holder | - | - | ATH16-16 | |
镗孔刀座Boring tool holder | - | - | BTH16-25 | |
快进速度 Rapidly travel | X轴快进速度X-axis rapid traverse | 15m/min | ||
Z轴快进速度Z-axis rapid traverse | 15m/min | |||
行程 Stroke | X轴行程X-axis travel | 320mm | ||
Z轴行程 Z-axis travel | 230mm | 270mm | 210mm(弹簧夹头)165mm(卡盘) | |
电机Motors | 主轴电机Spindle servo motor | 3.7/5.5kw | ||
进给轴(X/Z)电机Feed servo motors | 1.2kw | |||
其它 Etc | 总电气容量 Required electric power | 10KVA,AC200V±10%,50Hz | 8KVA,AC200V±10%,50Hz | 10KVA,AC200V±10%,50Hz |
机床尺寸(长×宽×高)Floor space | 1740×1410×1650mm | |||
机床重量Mass of machine | 约1800kg | 约1800kg | 约1900kg | |
(2)CNC装置标准规格CNC UNIT SPECIFCATIONS | ||||
控制系统Control unit | FANUC 0i TF | |||
控制轴数Controlled axis | 同时2轴(X/Z)、手动1轴 Simultaneously controllable 2axis, 1axis in manual mode | |||
输入方式Input system | MDI键入、绝对/增量值同时并用 MDI keyboard input、combined use of absolute/incremental programming | |||
程序记忆容 Part program storage length | 512KB | |||
插补功能 Interpolation function | 直线、锥面、圆弧、车螺纹Linear interpolation、pyramidal interpolation、Circular interpolation、threading interpolation | |||
最小设定单位Min. input increment | X:0.0001mm(直径) Z:0.0001mm | |||
最小移动单位Min. traverse increment | X:0.0005mm Z:0.001mm | |||
切削进给速度 Feed rate | 1~10000mm/min | |||
刀具补偿设定Tool offset | 64组Group | |||
辅助机能Auxiliary functions | M2、S4、T4 | |||
停顿时间 Dwell time | 0~99999.999S | |||
工进倍率Feed rate override | 0~150% | |||
快进倍率 Rapid traverse override | F0、25、50、100% | |||
输入输出接口Input/Output interface | RS232C/CF卡/USB | |||
显示语言 Display language | 中文、英语、日语Chinese、English、Japanese | |||
(3)其它规格OTHER SPECIFICATIONS | ||||
单一固定循环循环功能(G90,G92,G94) Canned cycles | 异常负荷检出功能 Unexpected disturbance torque detection | |||
英制/公制转换Inch/metric conversion | 可编程数据输入Programmable data input | |||
多重循环功能(G70-G76) Multiple repetitive cycles | 第二辅助功能(B代码) Custom macro B | |||
背景编辑 Background editing | 恒表面切削速度控制 Constant surface speed control | |||
加工时间,加工数量表示 Run hour and parts count display | 图纸尺寸直接输入 Direct Drawing dimension programming | |||
图形演示功能 Graphic function | 刀尖圆弧补偿 Tool nose radius compensation | |||
钻孔固定循环(G80-G89) Canned cycles for drilling | 螺纹加工回退 Threading retract | |||
变螺距螺纹车削(G34) Thread Cutting | 显示软盘程序目录 Directory display of floppy cassette | |||
宏指令Custom macro | 工件坐标系(G52-G59) Workpiece coordinate interpolation | |||
扩充程序编辑 Extended part program editing | 追加宏指令变量 Additional of custom macro common variables | |||
连续编号搜索 Sequence number search |
| |||
*由于产品不断更新,产品规格如有变化,恕不另行通知。 | ||||
VIEWO LIST
叶轮加工
100G样件加工-汽车零部件