NP Series
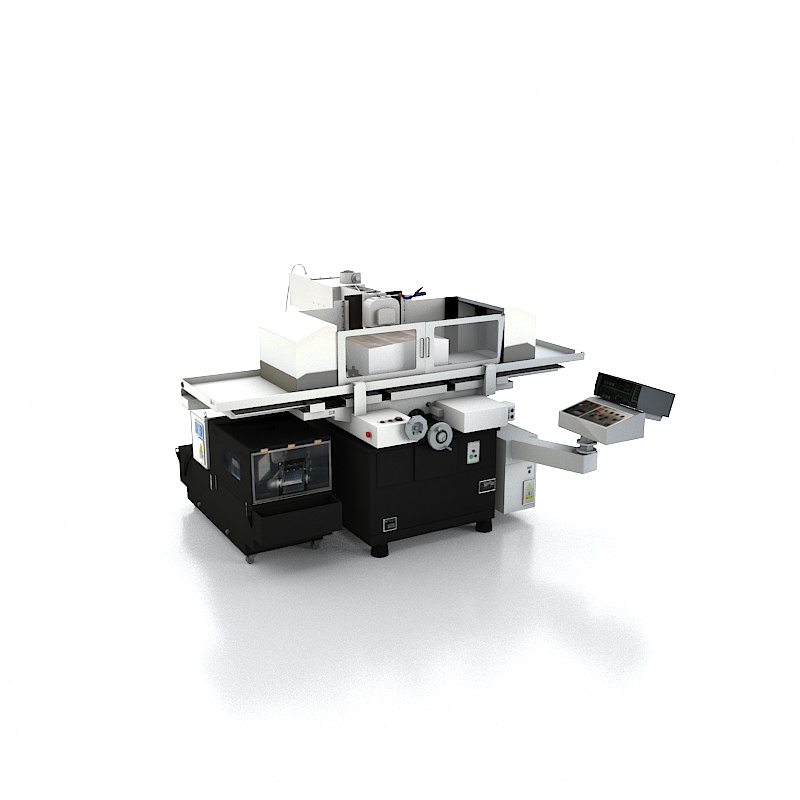
The left and right guide rails of the NP series high-precision forming surface grinder adopt a double V structure and a symmetrical structure to ensure the positioning accuracy of the machine tool. The standard configuration uses high-precision grating scales and actual position display for the upper and lower and front and rear axes.
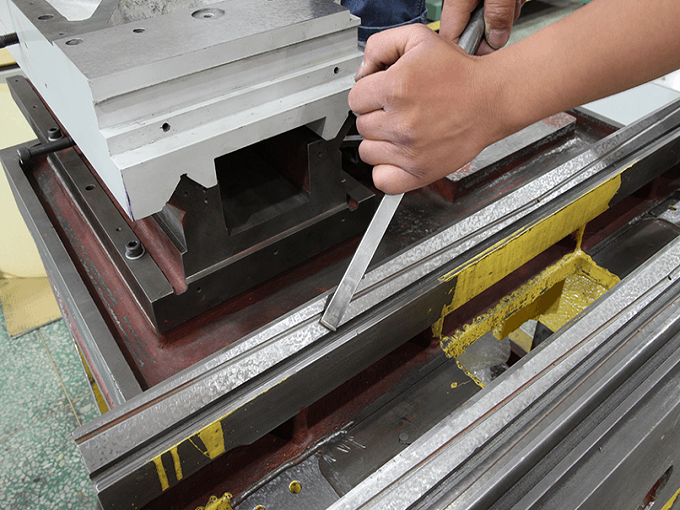
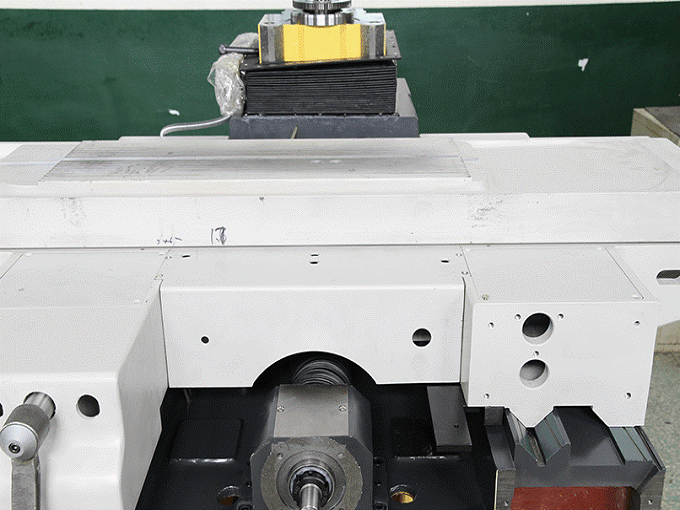
1.All guide surfaces of the machine tool are manually scraped

All the rail surface and the contact surface are manually scraped, and the scraping precision is within 2μm to ensure high precision.
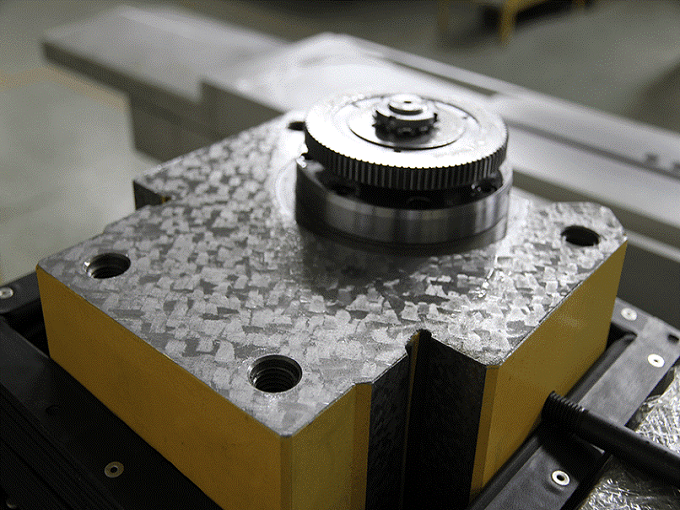
2.Column upper joint surface

All the rail surface and the contact surface are manually scraped, and the scraping precision is within 2μm to ensure high precision.
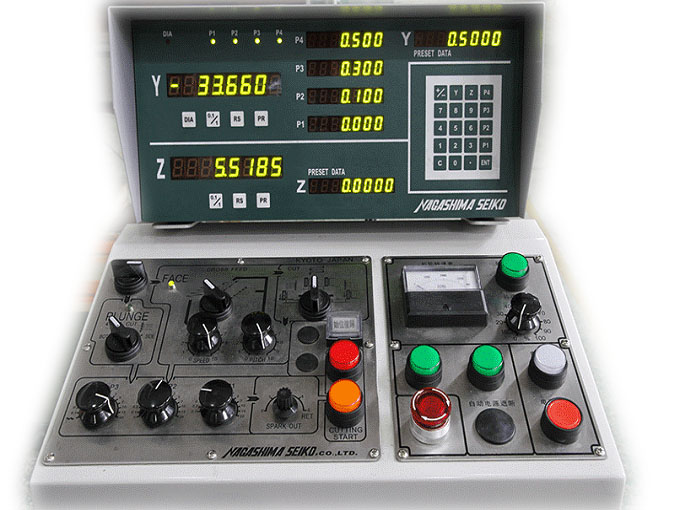
3.Operation panel and display

Large-size display, Chinese interface operation is extremely simple.
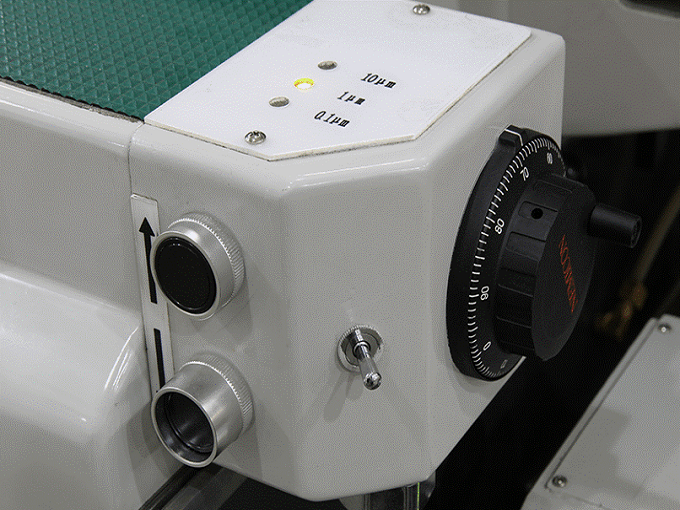
4.Quick lift button and electronic pulse handwheel

Wide adjustment range for fast movement.
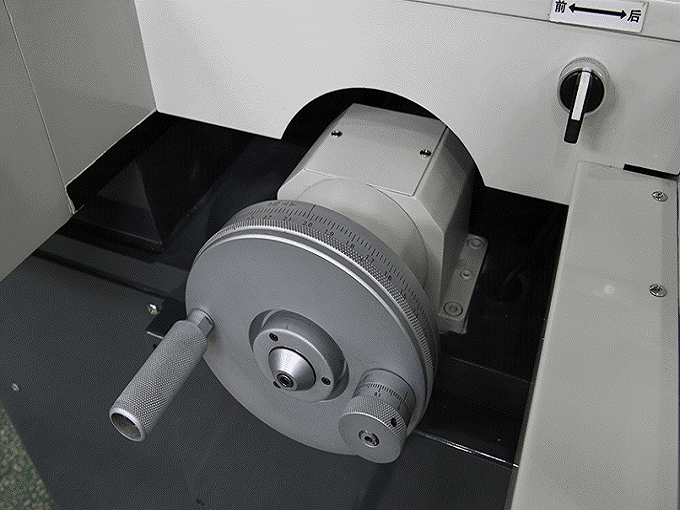
5.Adjustable front and rear feed handwheel

The minimum feed rate is 0.1μm, equipped with high-precision grating scale for closed-loop control and higher precision.
6.The guide rail surface adopts double V + double flat symmetrical structure

The structure is symmetrical, ensuring the positioning accuracy, high rigidity and stability of the machine tool.
7.Standard configuration and machine features
●The machine loading axis tracking precision and its accuracy of ± 1μm, guarantees an effective run without any major maintenance within 10 years, providing 30,000 hours of unpaid warranty.
●And that makes us the leader in the world market.
●The guide rail adopts our designed Double-V sliding guide rail structure, achieving an additional artificial precision that allows surface scraping to be made with higher precision, higher rigidity, higher vibration resistance and micron-scale accuracy.
●All our products are 100% designed and produce with Japanese Technology provided by Nagashima-Seiko.
●The upper, lower, front and back axis adopt a 1 um grinding precision with a 0.1 um of position control. And that makes us the leader in the world market.
●The guide rail and contact surfaces are treated with a manual scraping process,which is the only company in the world.
●Micron-grade feed grinding, achieving a level of 0.2 um in the grinding stage, and RY 0.3um in the mirror grinding stage.
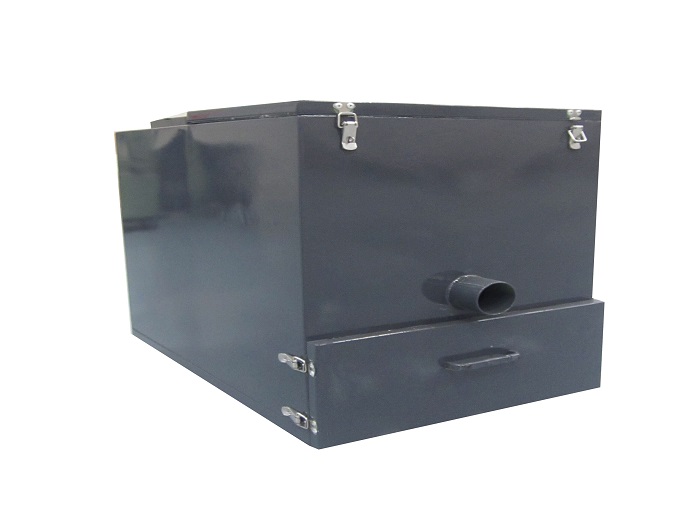
8.Vacuum cleaner
The fine sand and metal scraps splashed on the grinding wheel and the workpiece during grinding are collected to ensure the processing quality and environment.
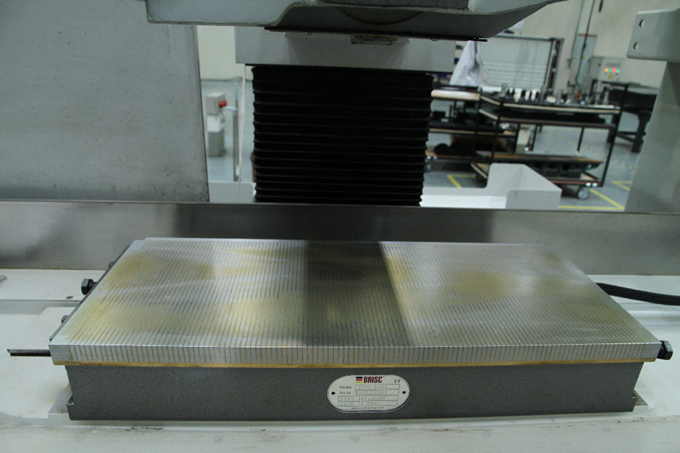
9.Electric permanent magnet plane magnetic table

High precision, no thermal deformation, energy saving.
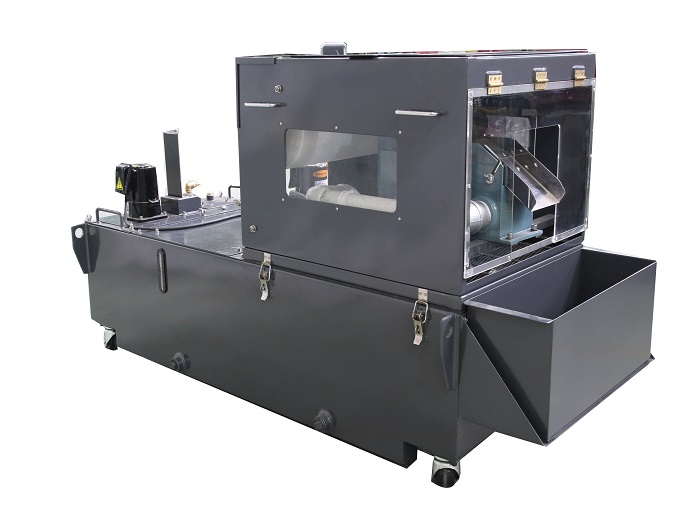
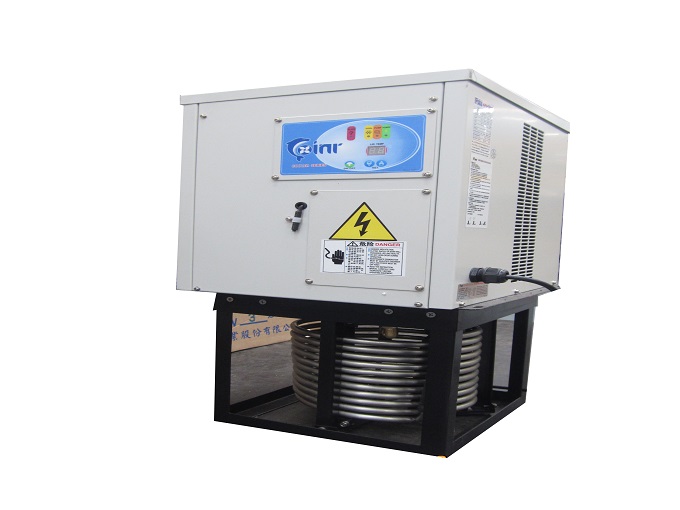
10.Cooling filter device

Properly reduce the temperature of the grinding surface and purify the coolant to improve processing efficiency and improve the working environment.

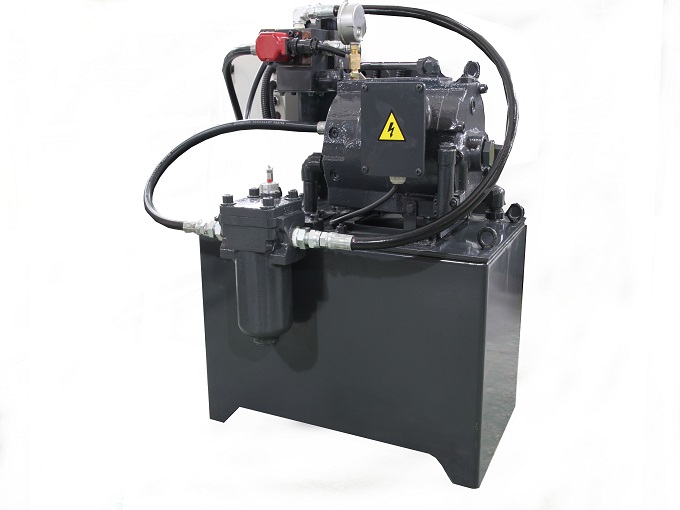
11.Hydraulic station device

It has reliable pressure retention, wide application, high efficiency and simple structure.
NP系列技术参数表 | |||||||||
项 目 | 单位 | NP520X-F | NP630X-F | NP640X-F | NP840X-F | NP1040X-F | |||
基本参数 | 控制系统 |
| NP-F | ||||||
显示器 |
| LED两轴数显器 | |||||||
工作台面尺寸(长×宽) | mm | 540×180 | 700×300 | 700×400 | 800×400 | 1000×400 | |||
工作台最大移动量 | 左右 | mm | 650 | 850 | 850 | 950 | 1150 | ||
前后 | mm | 230 | 340 | 440 | |||||
工作台面至砂轮主轴中心高度 | mm | MAX500 | |||||||
电永磁吸盘最大尺寸 | mm | 500×200 | 600×300 | 600×400 | 800×400 | 1000×400 | |||
床身底面距工作台上面距离 | mm | 1020 | 1080 | ||||||
加工工件最大重量(含电磁吸盘和修整器) | kg | 100 | 300 | ||||||
工作台(左右) | T型槽尺寸×槽数 |
| 12mm×1 | 12mm×2 | |||||
驱动方式 | 机械手轮一圈 | mm | 约90mm | 约90mm | 约90mm | 约90mm | 约90mm | ||
液压伺服驱动 |
| 有 | |||||||
机械手轮与液压伺服转换 |
| 手动 | |||||||
自动低速启动功能 | 有 | 有 | |||||||
液压驱动时移动速度 | m/min | 0~25 | 0~20 | ||||||
工作台(前后) | 手动进给 | 机械手轮 |
| 有 | |||||
大手轮旋转1圈 | mm | 4 | |||||||
小手轮最小刻度值 | mm | 0.01 | |||||||
最小显示值 | mm | 0.0001(0.1μm) | |||||||
自动进给 | 连续进给 | 进给速度 | mm/min | 0~450(无级变速) | |||||
断续进给 | 进给位置 |
| 工件左侧或左右两侧 | ||||||
进给量 | mm | 0~5 | |||||||
精磨时速度及进给量自动减半 |
| 有 | |||||||
高精度光栅尺 标准配置 | mm | 0.0001(0.1μm) | |||||||
数字显示器 标准配置 | mm | 0.0001(0.1μm) | |||||||
磨头 | 移动量 | mm | 350 | ||||||
快速进给速度 | mm/min | 450 | |||||||
手动进给 | 方 式 |
| 电子手轮3档倍率切换 | ||||||
手轮旋转1圈 | mm | 0.01/0.1/1 | |||||||
最小进给量 | mm | 0.0001/0.001/0.01 | |||||||
自动进给 | 总进给量 | μm | 任意设定量 | ||||||
精磨开始量 | μm | 任意设定量 | |||||||
每次进给量 | 粗磨 | μm | 0.1,0.2,0.3,0.5,0.7,1,1.5,2,3,5,7,10,15,20 | ||||||
中磨 | μm | 0.1,0.2,0.3,0.5,0.7,1,1.5,2,3,5,7,10,15,20 | |||||||
精磨 | μm | 0.1,0.2,0.3,0.5,0.7,1,1.5,2,3,5,7,10,15,20 | |||||||
进给位置 | 切磨(沟槽) |
| 工件左侧或左右两侧 | ||||||
纵磨(平面) |
| 工件前侧、后侧或前后两侧 | |||||||
无火花研磨次数 | 往复 | 0,1,2,4,6 | |||||||
高精度光栅尺 ( 标准配置) | mm | 0.0001(0.1μm) | |||||||
控制系统显示值( 标准配置) | mm | 0.0001(0.1μm) | |||||||
固定循环(标准配置) |
| 快速进给→粗磨→精磨→返回 | |||||||
| 粗→中→精→返回 | ||||||||
砂 轮 | 外径(最大)×宽(最宽)×内径 | mm | φ255×25×φ50.8 | φ305×32×φ76.2 | |||||
转 速 | rpm | 0~3600(无级变速) | 0~2400(无级变速) | ||||||
电 动 机 | kW | 2.2kW 4p | 7.5kW 4p | ||||||
润滑方式 标准配置 |
| 全自动润滑(油量不足自动检测) | |||||||
砂轮卡盘锥度 |
| φ33×1/6 | φ45×1/6 | ||||||
机床外形尺寸 长×宽×高 | mm | 约3100×2800×2100 | 约3900×3000×2100 | 约4050×3000×2200 | 约4050×3000×2200 | 约4200×3000×2200 | |||
机床重量 | kg | 约2000 | 约3500 | 约3700 | 约4000 | 约4400 | |||